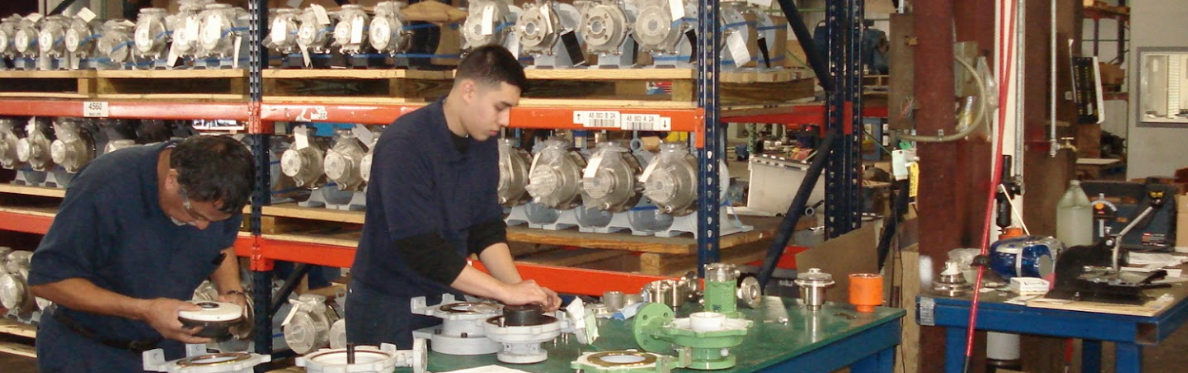
Delivering safe, leak-free, and high-performance pumping solutions to industries worldwide.
WHO WE ARE
"Since 1985 our passion has been your process reliability and profitability".
Magnatex Pumps, Inc. is a leading manufacturer of high-performance sealless magnetic drive and mechanical seal centrifugal pumps. Built to handle the toughest fluid handling challenges, our pumps deliver maximum operational uptime, zero emissions, and uncompromised safety in demanding environments.
From hazardous chemical transfer to high-temperature industrial processes, facility operators trust Magnatex to keep their operations running smoothly, efficiently, and safely.
Why Choose Magnatex:
- Sealless Safety & Zero Emissions: Our magnetic drive pumps eliminate mechanical seal failures, protecting workers, equipment, and the environment from toxic or costly fluid leaks.
- Heavy-Duty Construction: Built with premium materials—including metallic alloys and advanced fluoropolymer linings—to withstand severe corrosion, high pressures, and extreme temperature fluctuations.
- Lower Total Cost of Ownership: Engineered for low maintenance and long service life, reducing downtime and eliminating the routine upkeep associated with traditional mechanical seals.
- Proven Application Expertise: Decades of field experience allow us to help you select the exact pump configuration for your specific process requirements.
Our Service Capabilities
At Magnatex, our support goes far beyond delivering a pump. We partner with you through every phase of your system's life cycle:
- Custom Application Engineering: Tailored pump selection to match flow, head, temperature, and chemical compatibility requirements.
- Extensive Inventory & Rapid Delivery: Comprehensive stocking of complete pump units and genuine replacement parts to minimize your facility's unplanned downtime.
- Comprehensive Technical Support: Dedicated technical teams ready to assist with system troubleshooting, installation guidance, and operational optimization.
- Spare Parts & Assemblies: Easy access to drop-in replacement assemblies and spare components for fast, straightforward maintenance.
Industries & Applications Served
Magnatex pumps are engineered to excel across a wide range of demanding sectors:
- Chemical & Petrochemical Processing
- Industrial & Municipal Wastewater
- Pharmaceutical & Specialty Chemical Manufacturing
- General Industrial Process & Fluid Handling
- Corrosive & High-Temperature Chemical Transfer
Ready to Optimize Your Fluid Handling System?
Partner with Magnatex for dependable, leak-free pumping solutions tailored to your process.